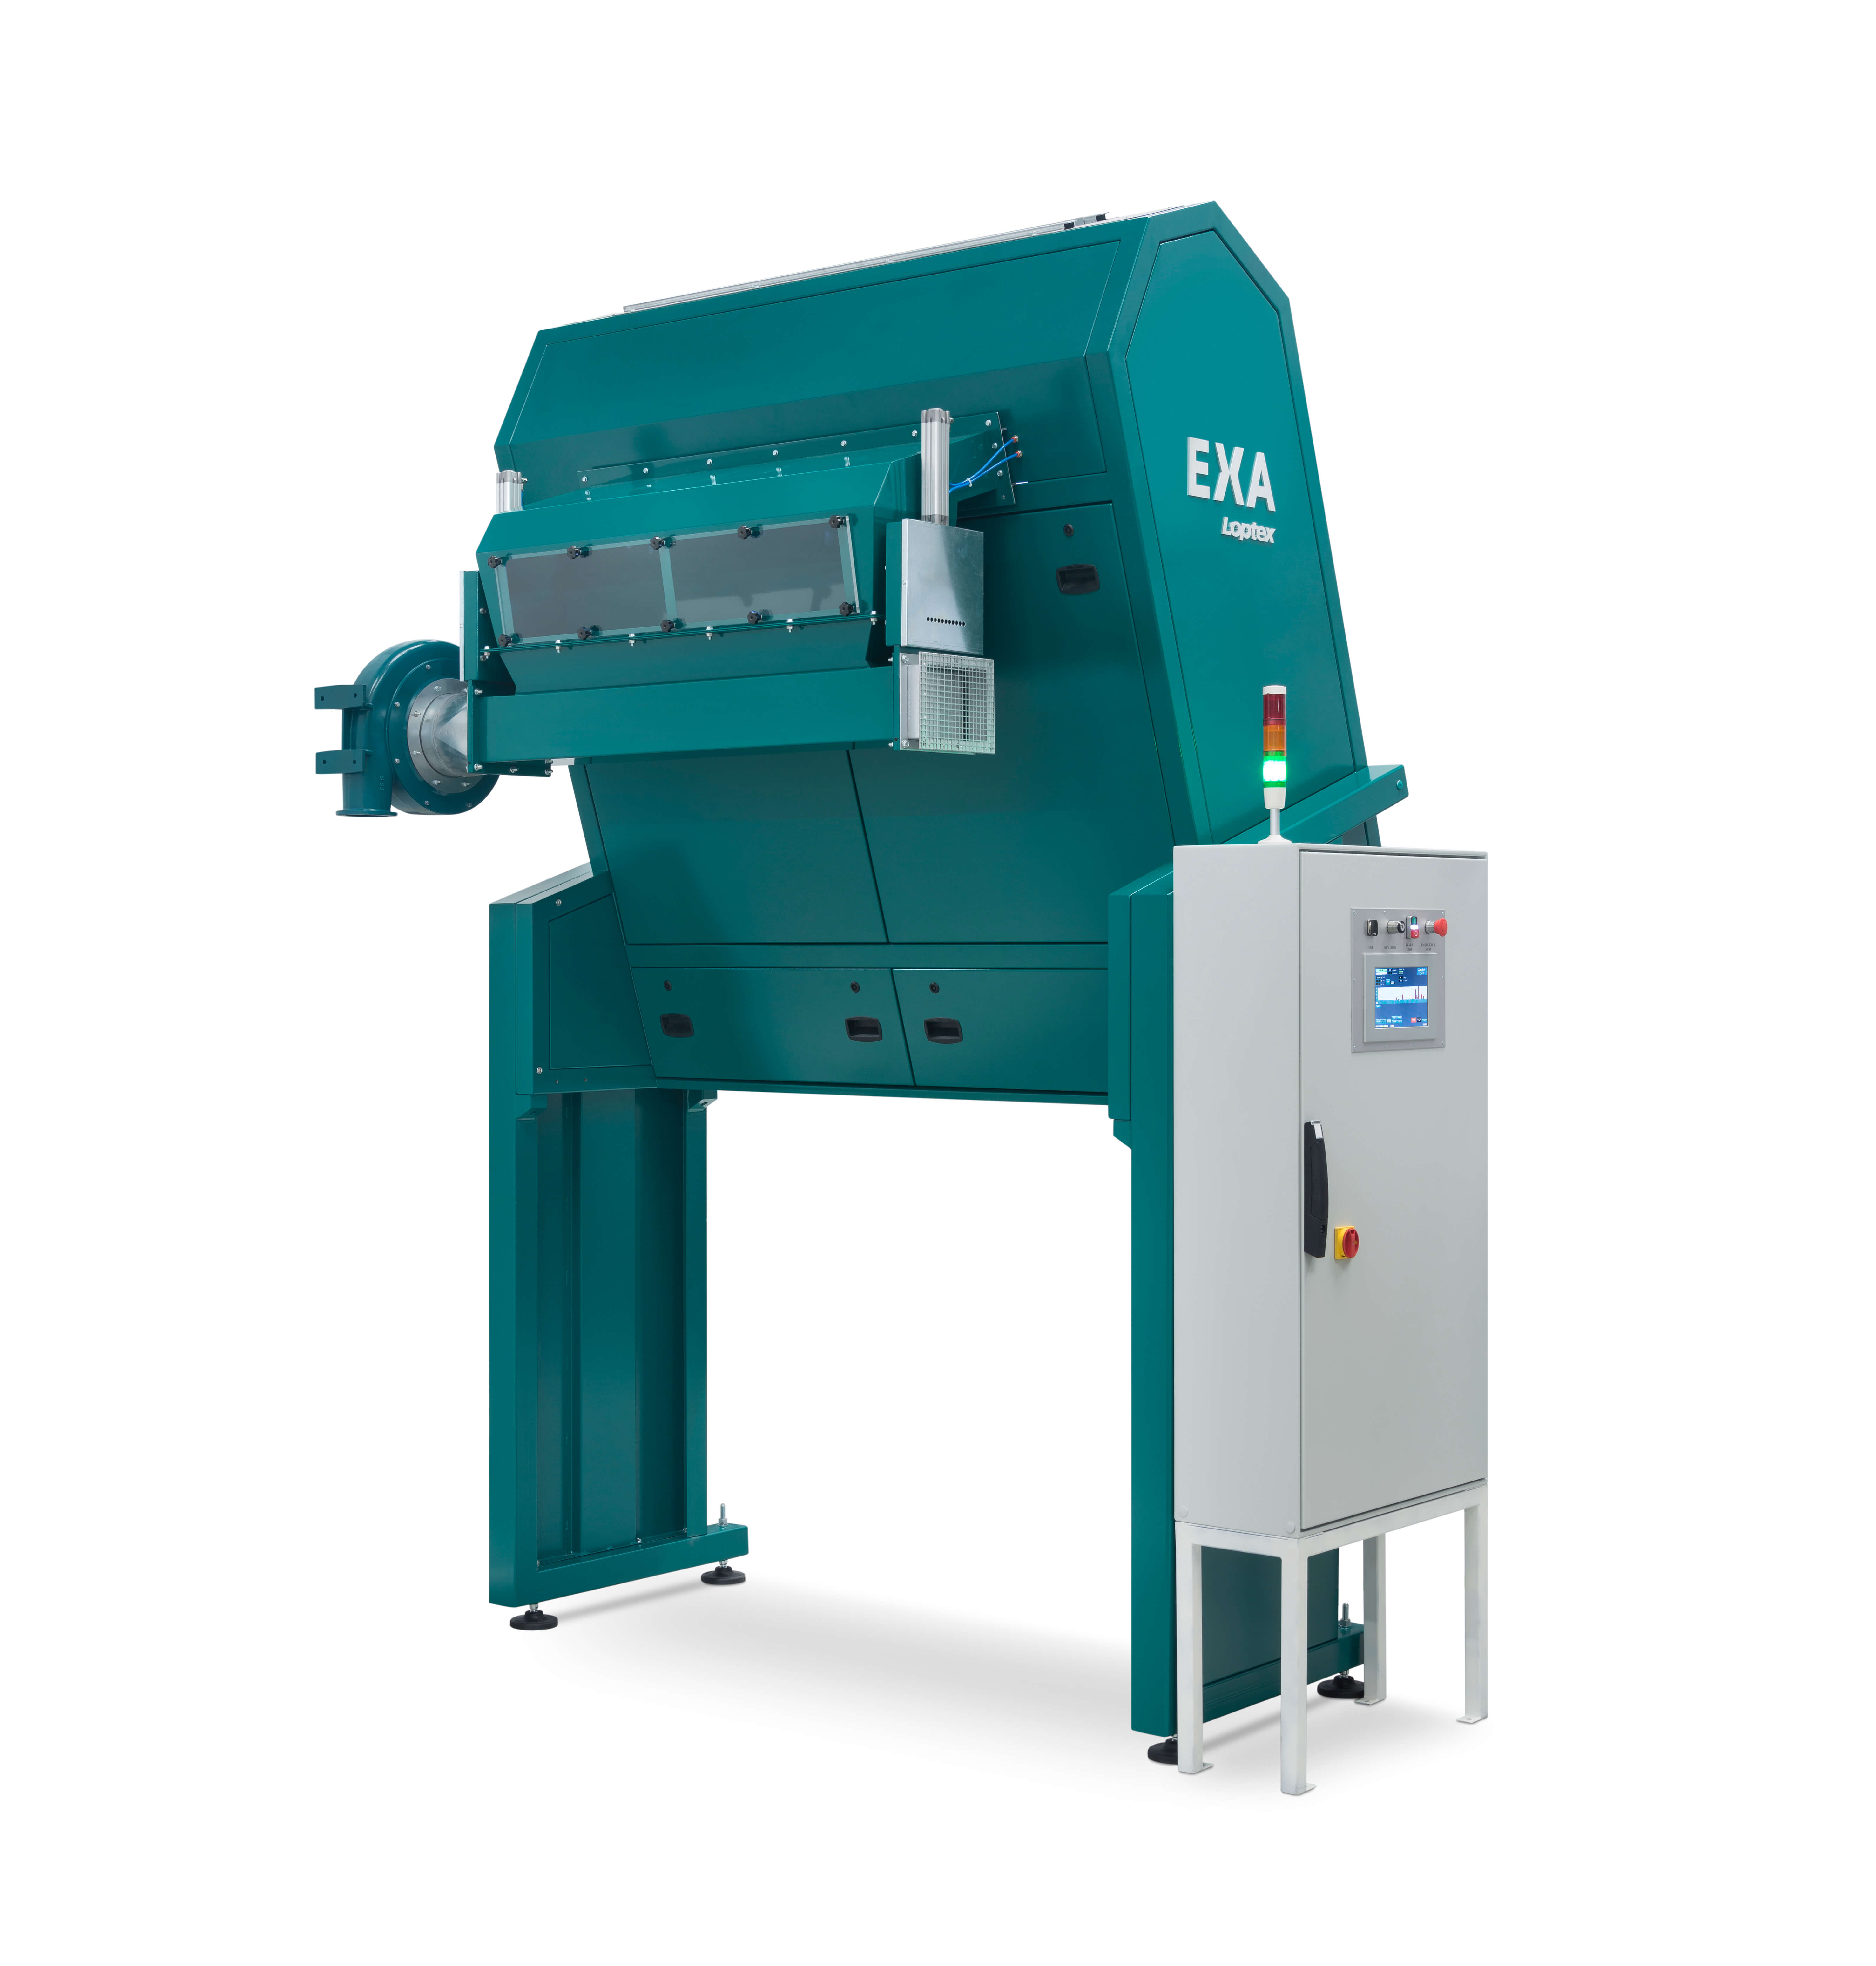
Loptex, a leading manufacturer of quality monitoring systems, is exhibiting its new technological concept of its EXA products line at Innovate Textile & Apparel.
The contamination content in raw materials is still a serious issue. And with consumers becoming increasingly aware of this problem, a solution needs to be found, especially considering that these materials sit on our skin and contribute to our comfort and wellbeing.
With this in mind, Loptex offers state-of-the-art and proven solutions for the textile industry to implement a zero-contamination strategy through its EXA products.
“Loptex EXA includes a new product line for applications in spinning and nonwovens,” the company says.
“EXA, by means of multiple embedded camera systems and specific illumination, detects, classifies and eliminates all types of contaminants during the industrial process.”
Specifically, Loptex UV-R embedded technology combined with red and ultraviolet light, identifies optically brightened and shiny contaminants that are invisible on the raw processing material.
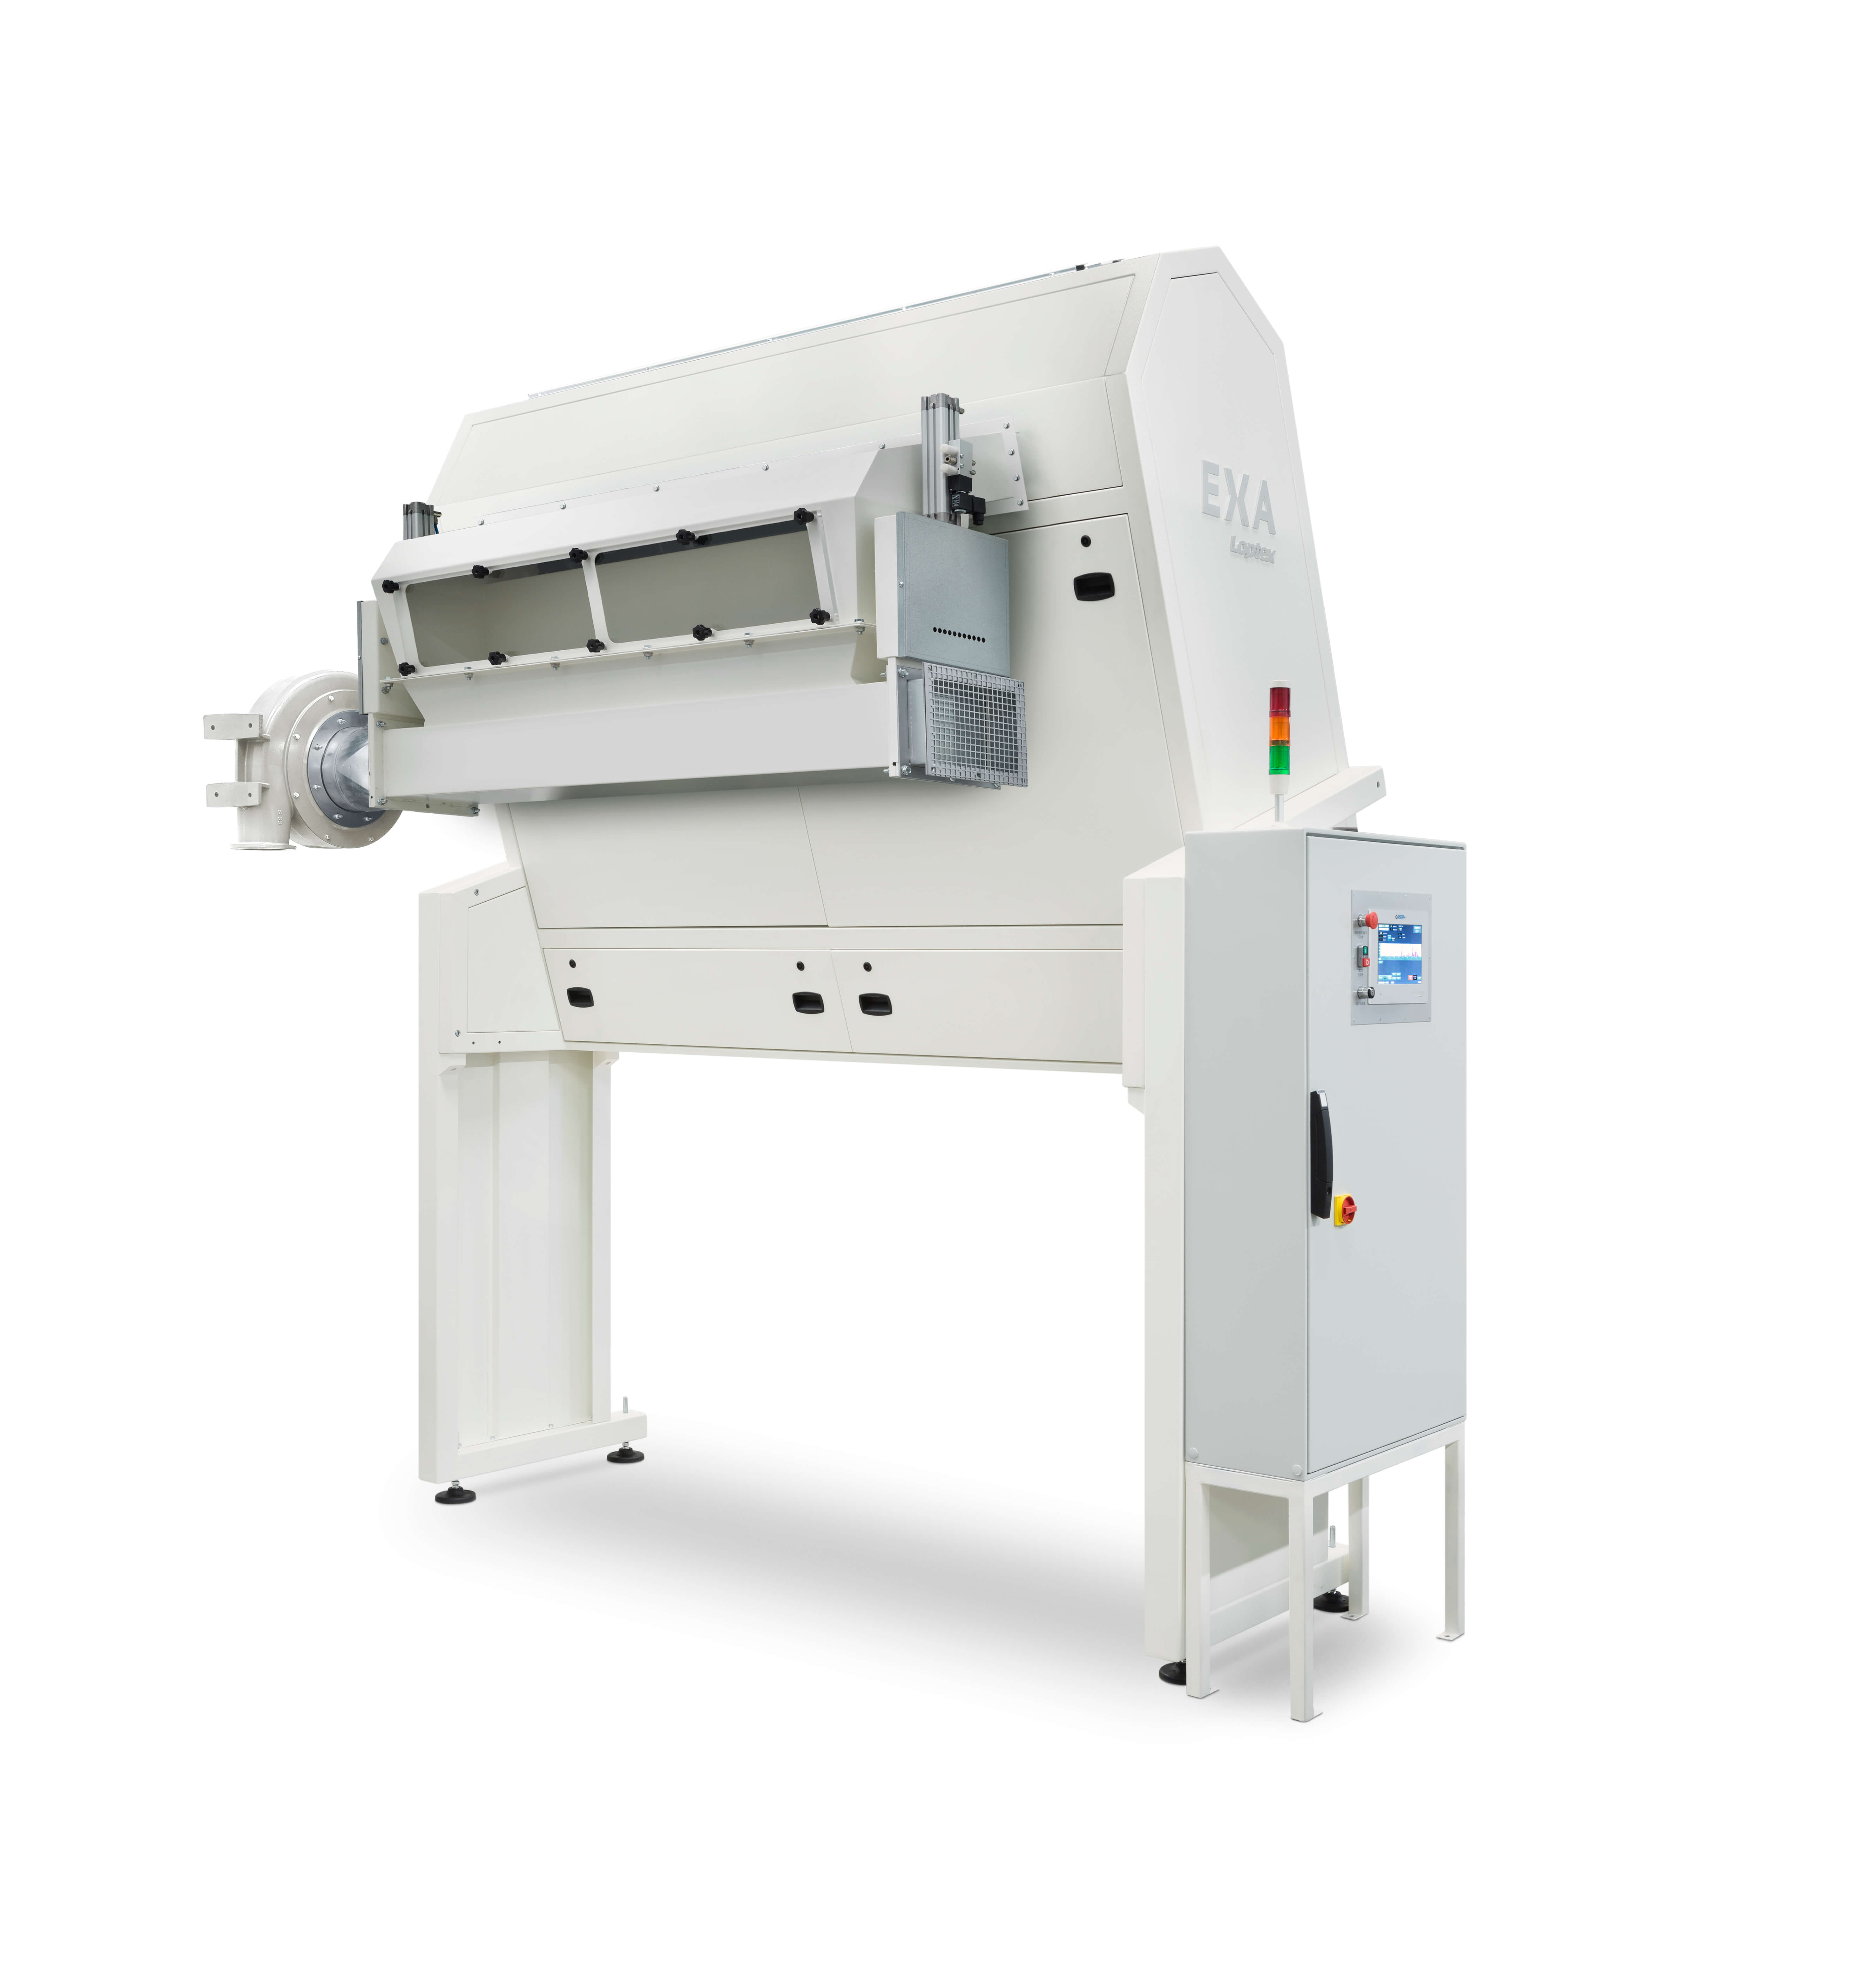
The coupling of EXA with UV-R technologies meet the highest quality standards granting the comprehensive elimination of contaminants including colourless and white polypropylene (PP).
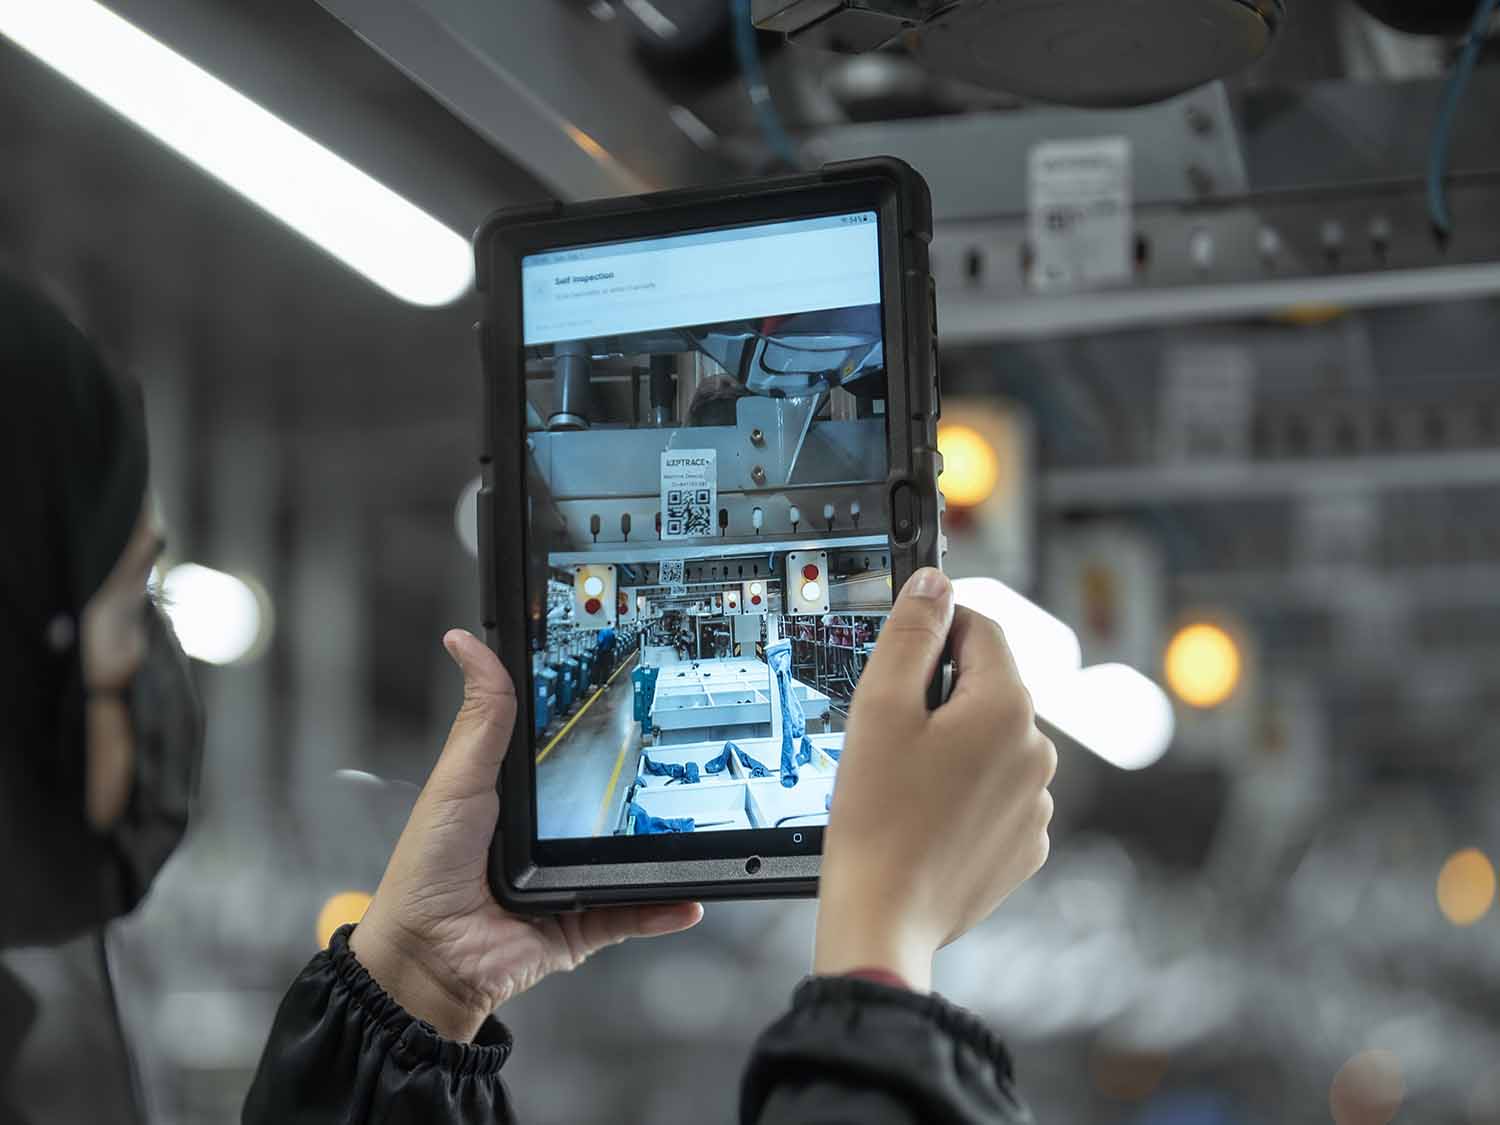
The company adds: “Industry 4.0 is the new industrial revolution which, through a digitalisation process, combines know-how, technologies and human resources for the optimisation of the value chain. EXA’s cutting-edge digital embedded technology helps to fill this competence gap in the production process.”
What's more, the remote-control option enables the optimisation of settings and calibration providing full assistance to the operator. It also features predictive maintenance analysis and online control of components.
Furthermore, the EXA CLASS, data acquisition and contamination classification system, offers statistical data which is helpful for optimising the process and guaranteeing the comprehensive control of quality.